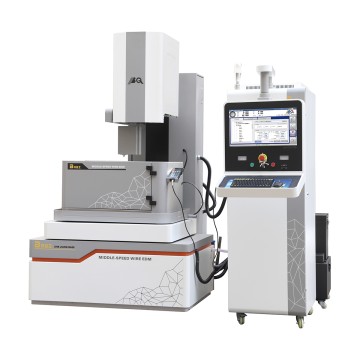
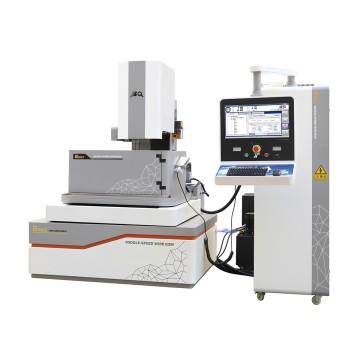
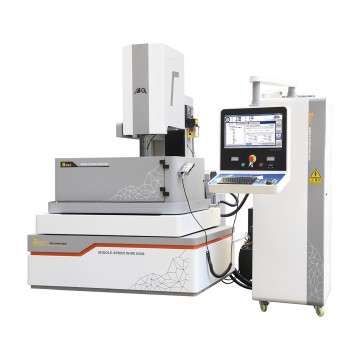
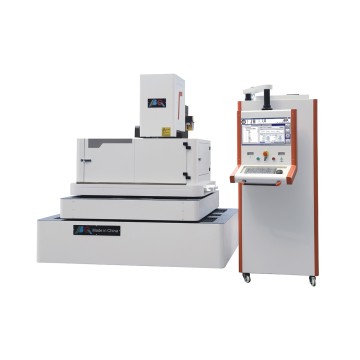
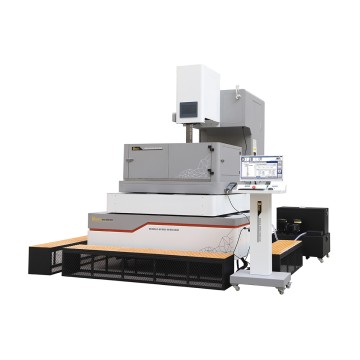
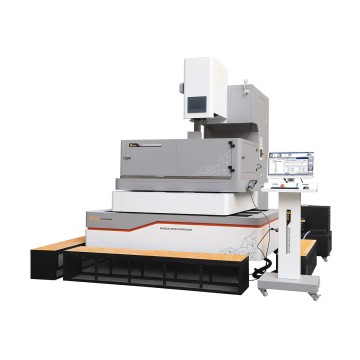
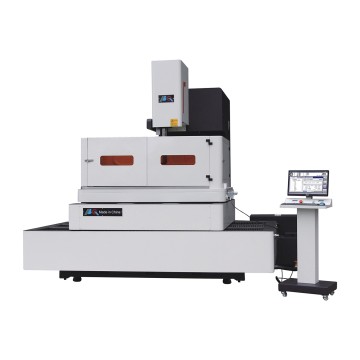
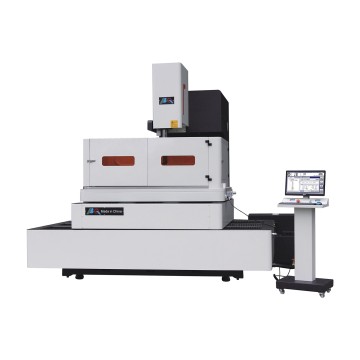
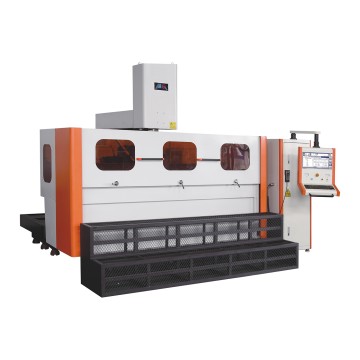
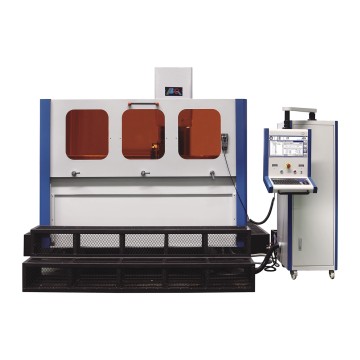
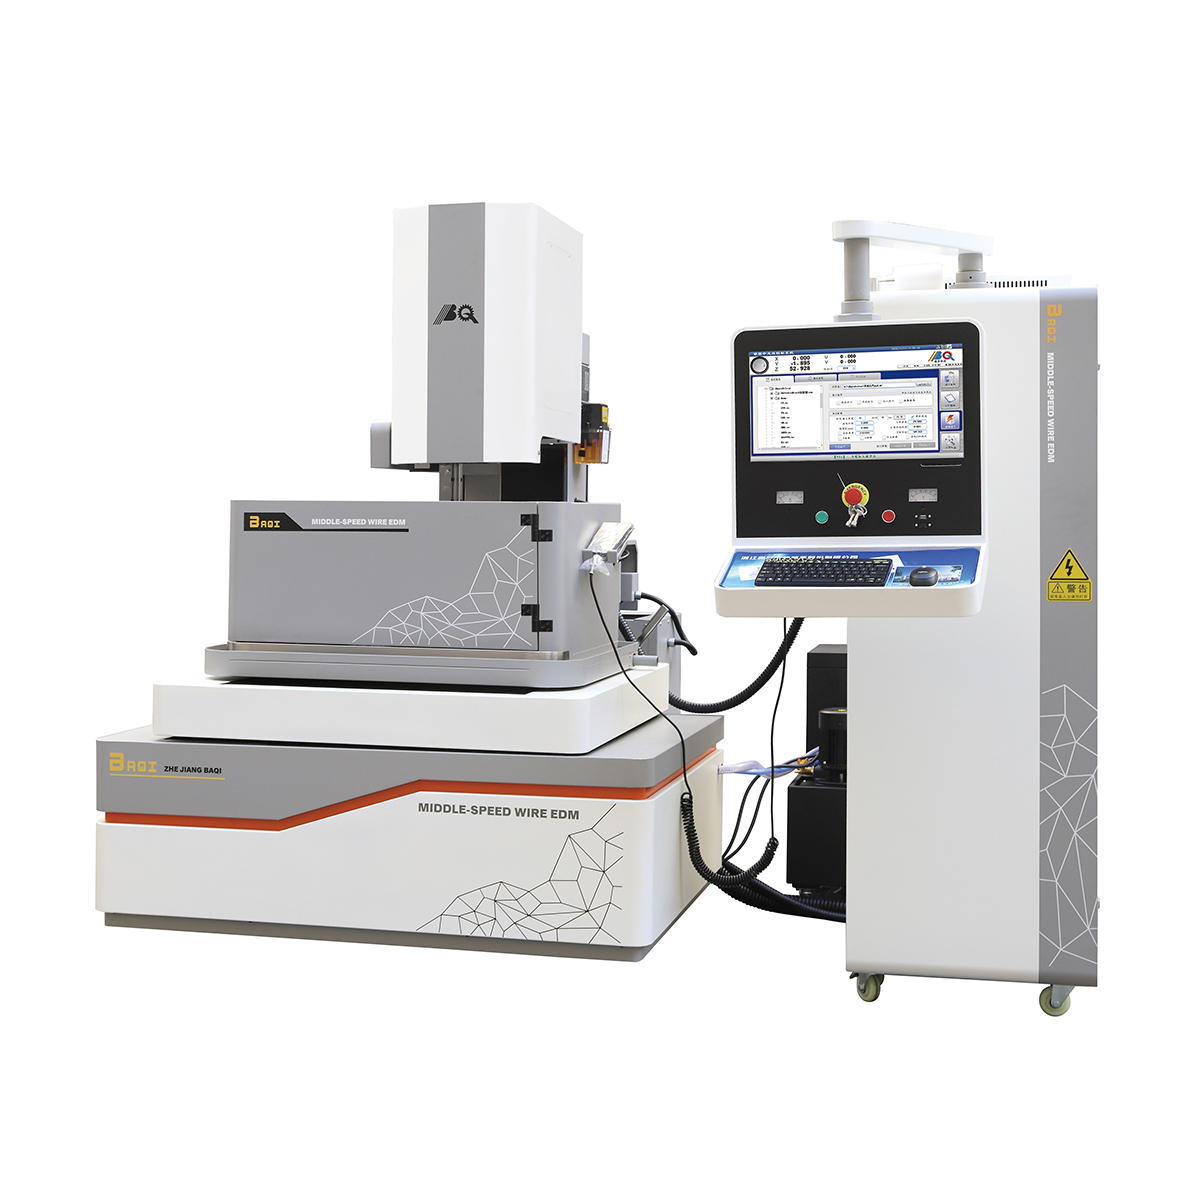
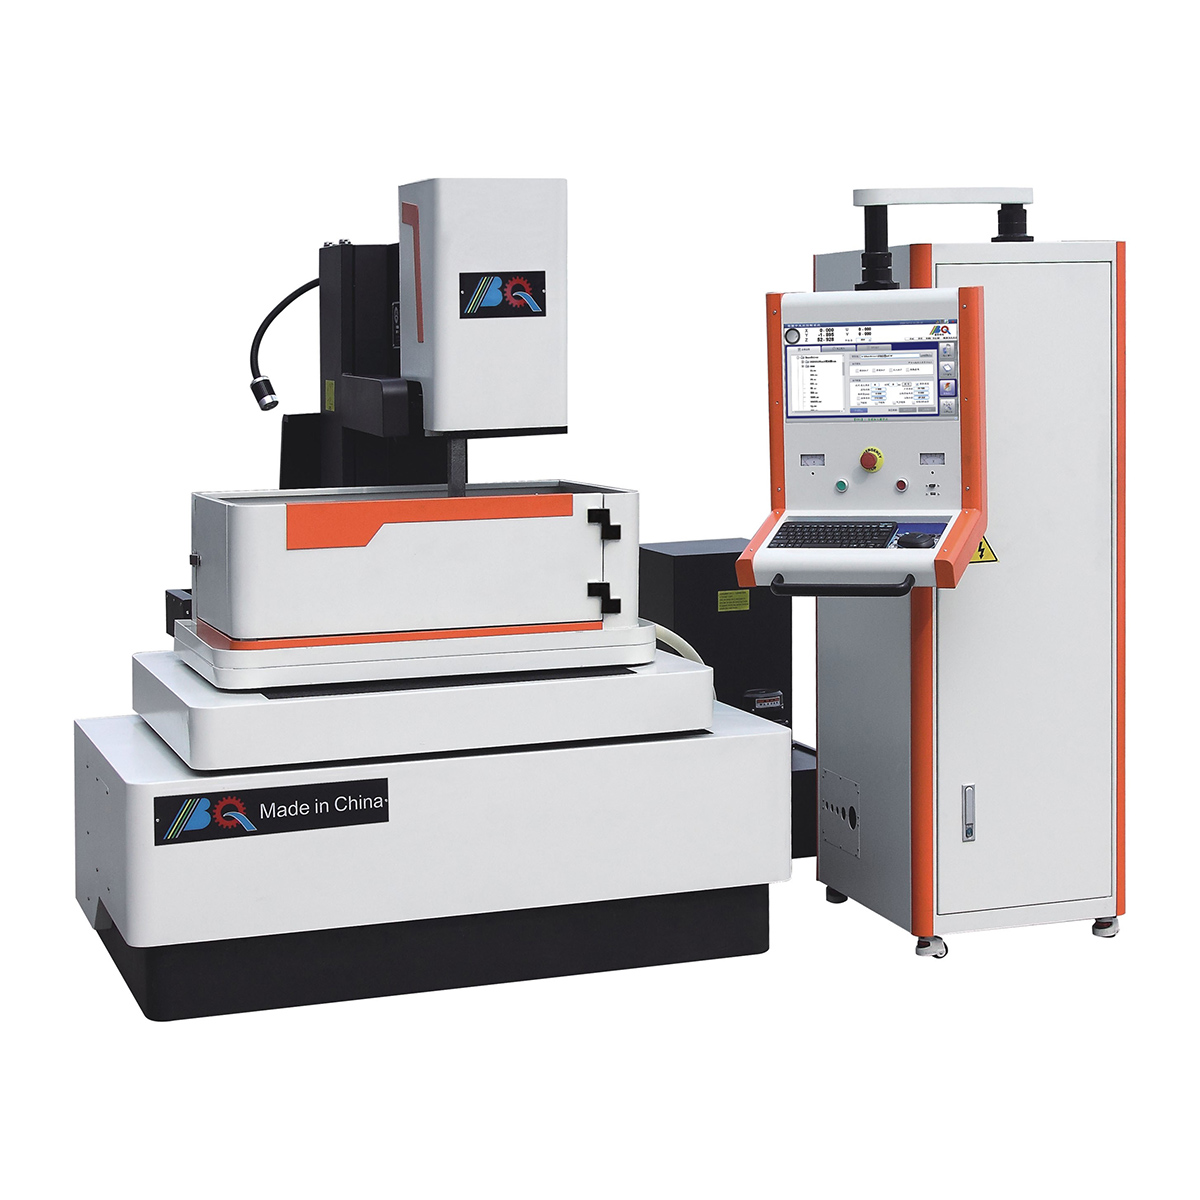
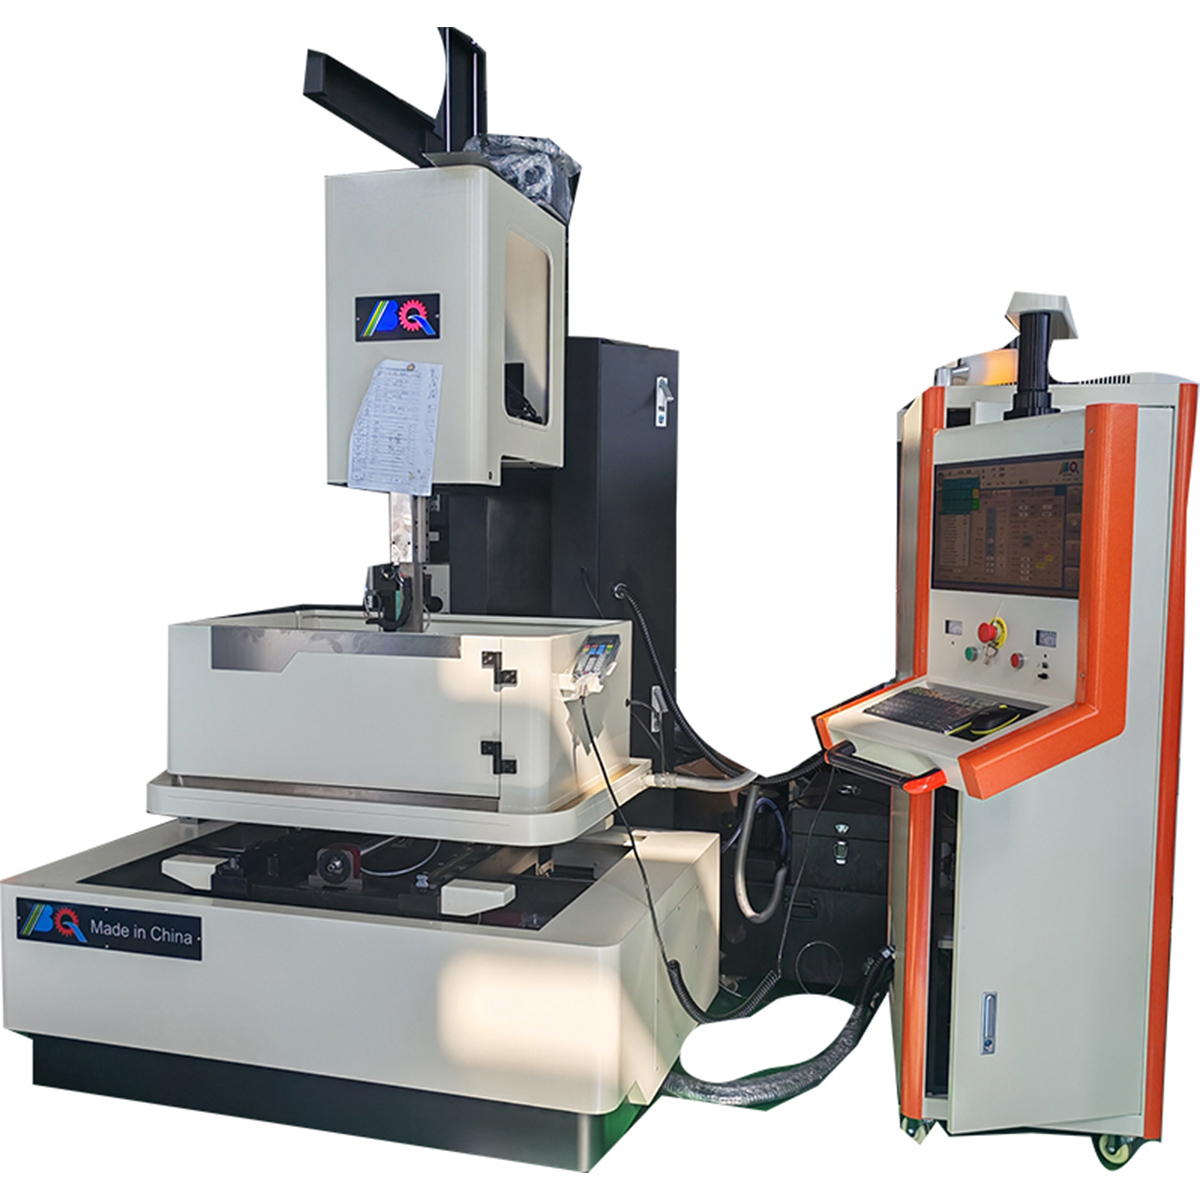
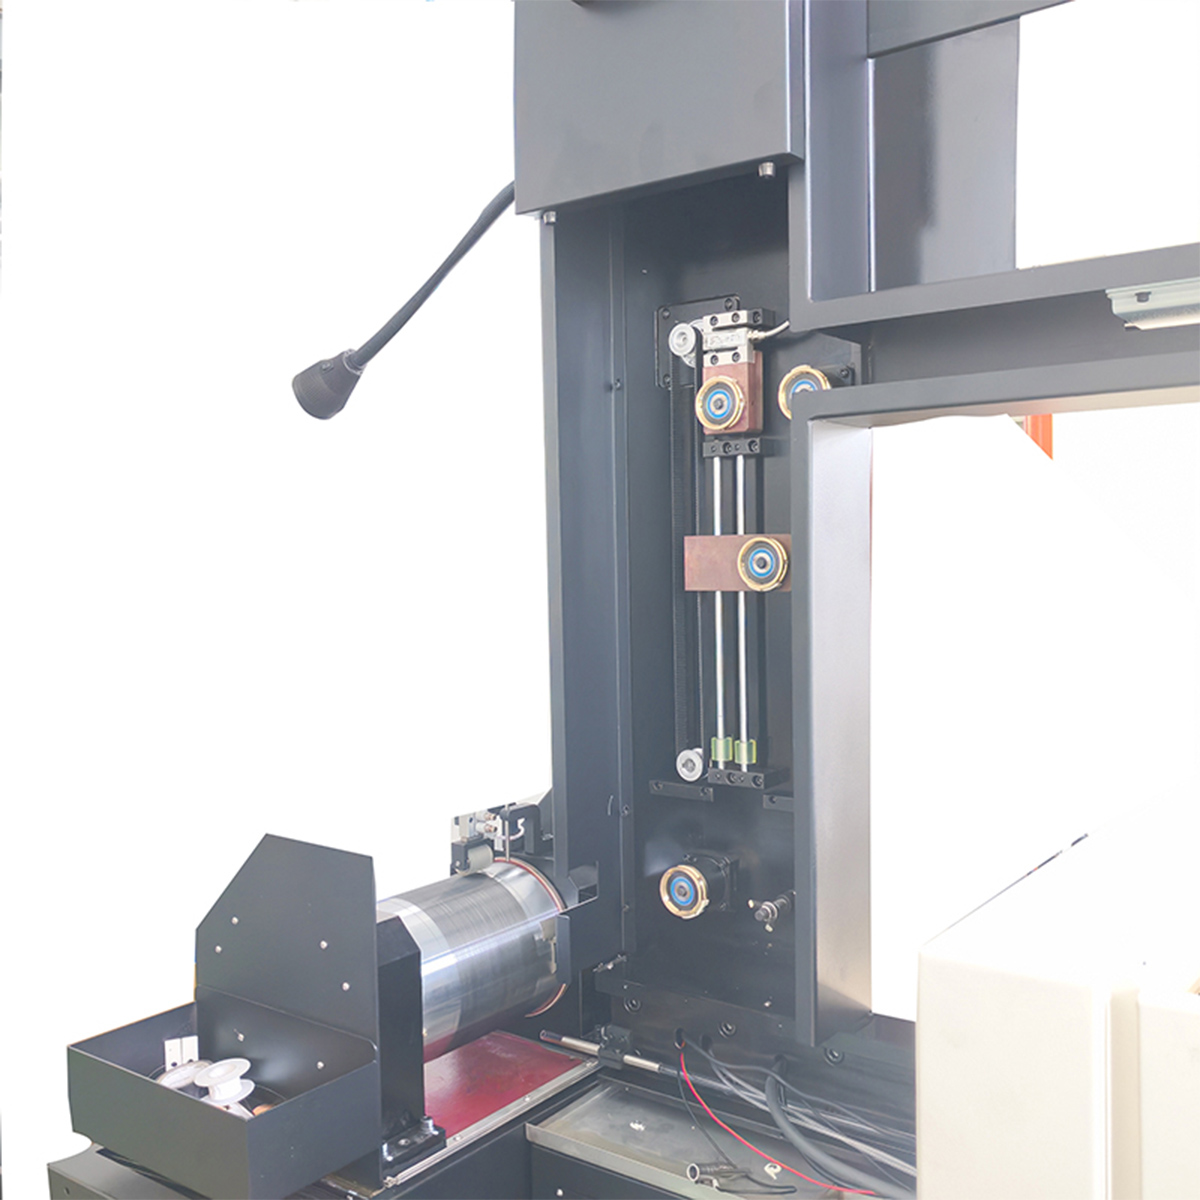
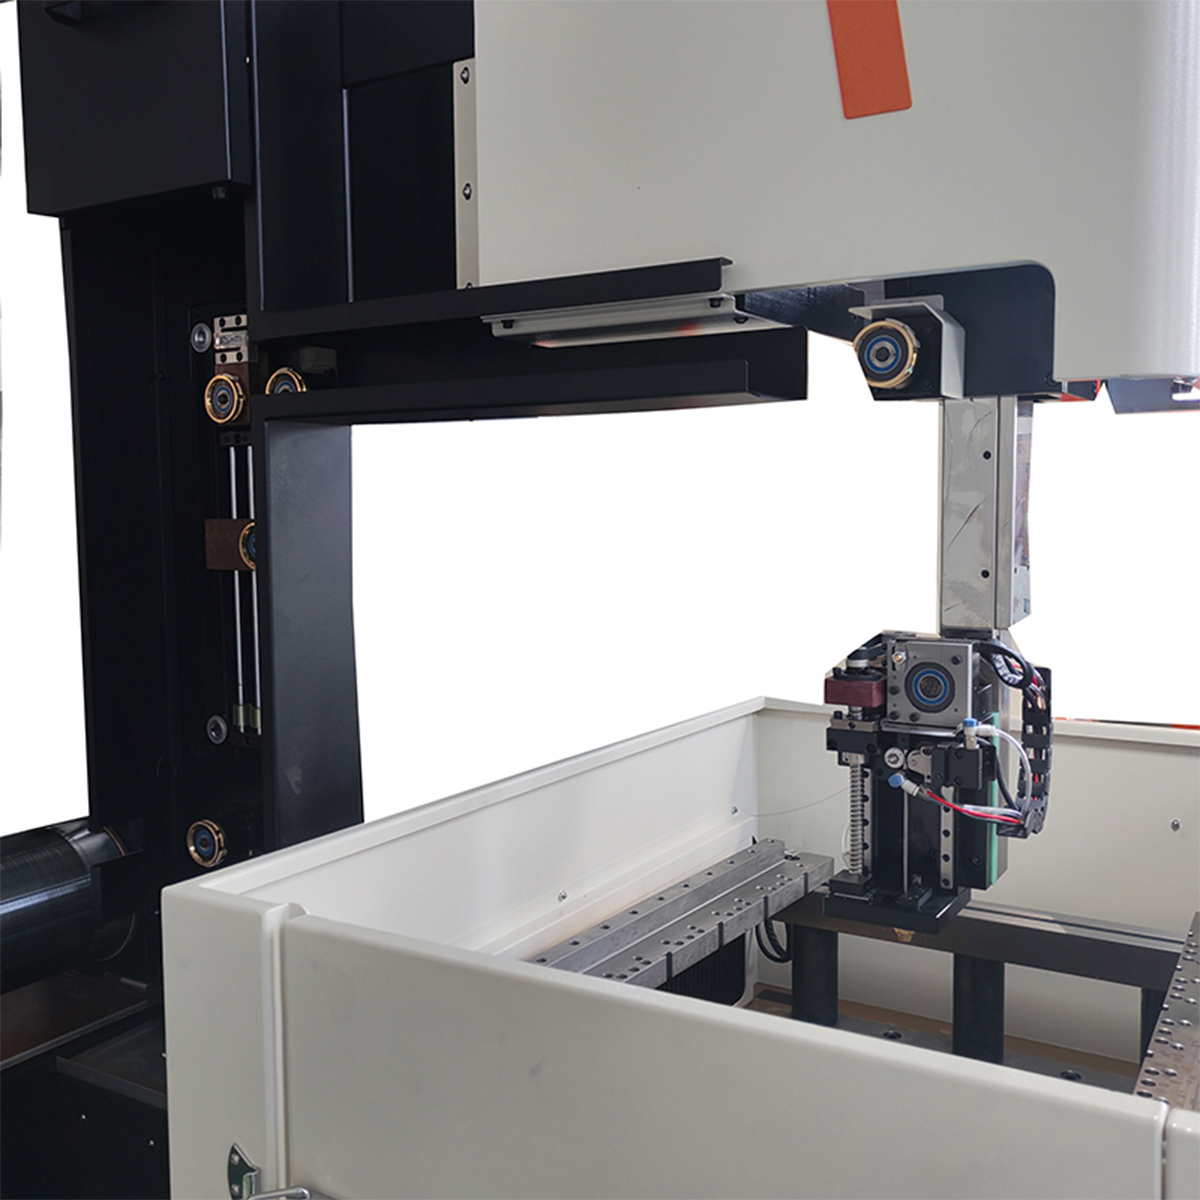
High Precision 5 Axis linkage BQ500 Medium-Speed CNC Wire cutting EDM Machine
Share to:


Model |
BQ500 |
|
Table travel |
Worktable size(mm) |
756×590 |
X/Y travel (mm) |
500×400 |
|
Max work piece size(mm) |
900×600 |
|
Max cutting thickness (mm) |
300 |
|
Max load weight (kg) |
600 |
|
X/Y min.directive unit(mm) |
0.001 |
|
Taper and Z-axis travel |
Taper U/V travel (mm) |
80×80 |
Max cutting taper (mm) |
±15°/150 mm |
|
U/V min.command unit(mm) |
0.001 |
|
Transmission control |
Control method |
X/Y/U/V/Z Servo driven(Linear motor are option for X/Y) |
Z axis drive |
Numerical control |
|
Simultaneously controlled axes |
X Y U V-4 Axis |
|
Wire drum |
Max travel of wire drum(mm) |
200 |
Wire diameter(mm) |
①0.1-Φ0.2 (Standard 0.18) |
|
Wire speed(m/s) |
1-11.4 variable frequency |
|
Max.wire storage length (m) |
330 |
|
Machining parameters |
Reposition accuracy(mm) |
≤±0.003 |
Max cutting efficiency(mm²/min) |
≥300 |
|
Roughness/Ra(μm)cut 1 trim 2 |
0.7-1.4 |
|
Working liquid tank |
Liquid tank capacity |
120L |
Filtering method |
3 Layer filtration |
|
Others |
Power supply |
Three phase 380V AC/5OHz |
Control System |
Baqi system |
|
Total power consumption (kw) |
1.7 |
|
Max machining current(A) |
10 |
|
Machine gross weight(kg) |
2600 |
|
Machine size(mm) |
1540x1760×2080 |
|
Machine noise |
≤70dB |
|
Top-bottom irregular cutting |
Yes |
Baqi Intelligent's Medium-Speed Molybdenum Wire EDM are widely used in various fields such as mold and tooling, medical industry, aerospace, automotive parts, machining, military defense, and more. Let's explore the application characteristics and advantages of medium-speed wire cutting machines in different industries:
Application and Advantages of Medium-Speed Molybdenum Wire EDM Machines in the Injection Mold Industry
Medium-speed molybdenum wire EDM machines (medium-speed wire EDM) are economical and efficient precision machining equipment in injection mold manufacturing. Using a reciprocating molybdenum wire as the electrode, they remove metal through electrical discharge, achieving high-precision cutting of complex contours. They achieve a golden balance between precision, efficiency, and cost, and are widely used for precision machining of key parts such as injection mold cavities, cores, inserts, sliders, and ejector pin holes. They are particularly adept at handling high-hardness, complex, and irregularly shaped mold parts after quenching, making them an essential core processing equipment for modern injection mold factories.
Application in the Injection Mold Industry
1. Core Machining Objects
●Core Molding Parts: Cavities, Cores, Inserts, Mold Cores (key components determining the appearance and dimensions of injection molded products).
●Moving Structure Parts: Slider, Angled Ejector, Core Pulling Mechanism, Guide Parts (for complex undercuts and side hole molding).
●Precision auxiliary holes: ejector pin holes, guide pin holes, positioning holes, cooling water holes (to ensure mold assembly accuracy and smooth movement).
●Complex features: deep cavities, narrow slits, small R-angles, variable sections, draft slopes, upper and lower profiles (structures that are difficult to machine with traditional milling).
2. Core Process Positioning
Wire EDM is a key process in the finishing of injection molds after heat treatment. The standard process chain is: CNC roughing → quenching (HRC 52-58) → wire EDM finishing → grinding/polishing → assembly. It is mainly responsible for ensuring the final dimensional accuracy, form and position tolerance, fit clearance and surface quality of the parts, which directly affects the mold life and the quality of injection molded products.
3. Applicable Mold Types
●Home appliance / Digital molds: mobile phone shells, chargers, home appliance shells, monitor bezel molds.
●Automotive interior molds: dashboards, door panels, center console panels, connectors, buckle molds.
●Precision electronic molds: connectors, micro gears, sensor shells, thin-walled part molds.
●General plastic molds: daily necessities, toys, packaging, medical consumables molds.
4. Industry Penetration
Domestic injection mold factories have a penetration rate of over 90%, making it the main equipment for small and medium-sized mold factories and the first choice for economic processing for large mold factories. Used for non-mirror, non-ultra-high precision parts (over 90% of injection mold requirements), replacing some wire EDM to achieve cost reduction and efficiency improvement.
Core Advantages of Wire EDM in Injection Molds
1. Extreme Cost-Effectiveness: Low Cost, High Precision
● Low Equipment Investment: Price is 1/3 to 1/5 of that of wire EDM, low investment threshold, and fast return on investment.
● Extremely Low Consumable Material Consumption: Molybdenum wire is used repeatedly, and wire consumption is only 1/10 of that of copper wire in wire EDM, reducing overall processing costs by 60%+.
● Precision meets standards: After multiple cuts (1 rough cut + 2~3 fine cuts), the dimensional accuracy is ±0.003mm and Ra is 0.8~1.6μm, which meets the requirements of most injection mold fitting clearance (0.01~0.03mm) and lifespan.
2. Hard Material Machining: First Quenching, Then Cutting, Zero Deformation
● It can directly machine high-hardness mold steels such as S136, 718H, NAK80, and P20 with HRC 52-58 after quenching, without tool wear.
● First quenching, then cutting, completely eliminates heat treatment deformation, ensuring stable cavity and core dimensions, uniform gaps, and long-term durability.
3. Stress-Free Machining: First Choice for Complex Structures and Thin-Walled Parts
● Non-contact machining, no cutting force, perfectly machining slender cores, thin ribs, deep cavities, cantilevered parts, irregular undercuts, and other easily deformable structures.
● Sharp corners (R≤0.05mm) and precise contours reduce polishing workload and improve the appearance quality and demolding smoothness of injection molded products.
4. High Efficiency and Flexibility: Adaptable to Multiple Varieties and Small Batches
● Overall efficiency is 30%~40% faster than wire EDM, supporting 24-hour unattended continuous operation.
● One-click programming, quick part change, no special tools required, adaptable to the production characteristics of injection molds with multiple varieties, small batches, and frequent mold changes.
5. Comprehensive Functions: Taper Cutting, Adaptable to Complex Structures
● Four-axis linkage, capable of cutting ±6°~15° draft angle, slider guide post holes, and cavity taper, reducing secondary processes.
● Equipped with automatic wire tightening, wire breakage protection, automatic center finding, and upper and lower irregular shape cutting, adaptable to complex mold structures, high stability, and easy operation.
Illustrations
Figure 1: Medium-Speed Molybdenum Wire EDM Machine
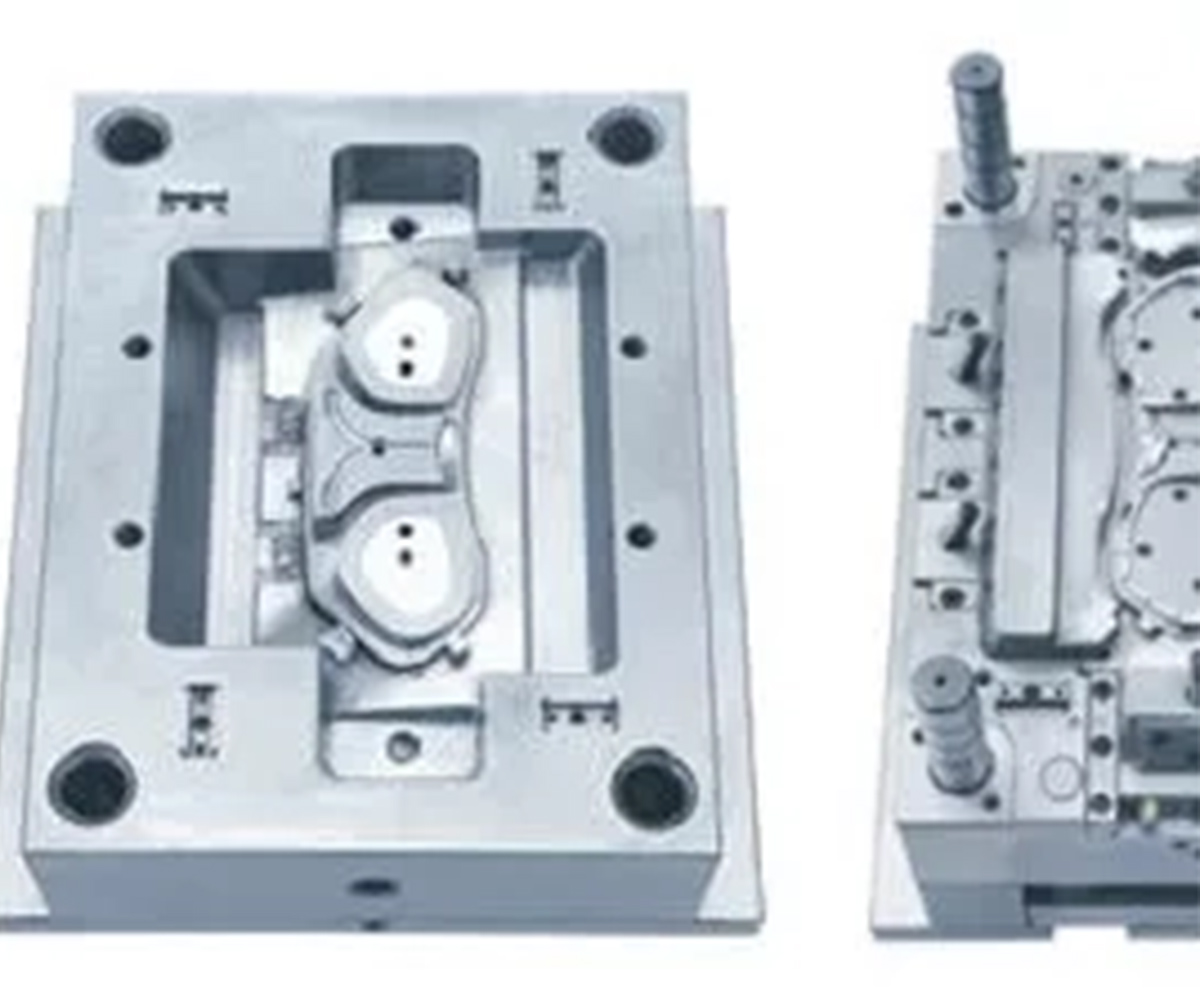
Figure 2: Injection Mold Cavity / Core Insert Machined by Medium-Speed Wire EDM
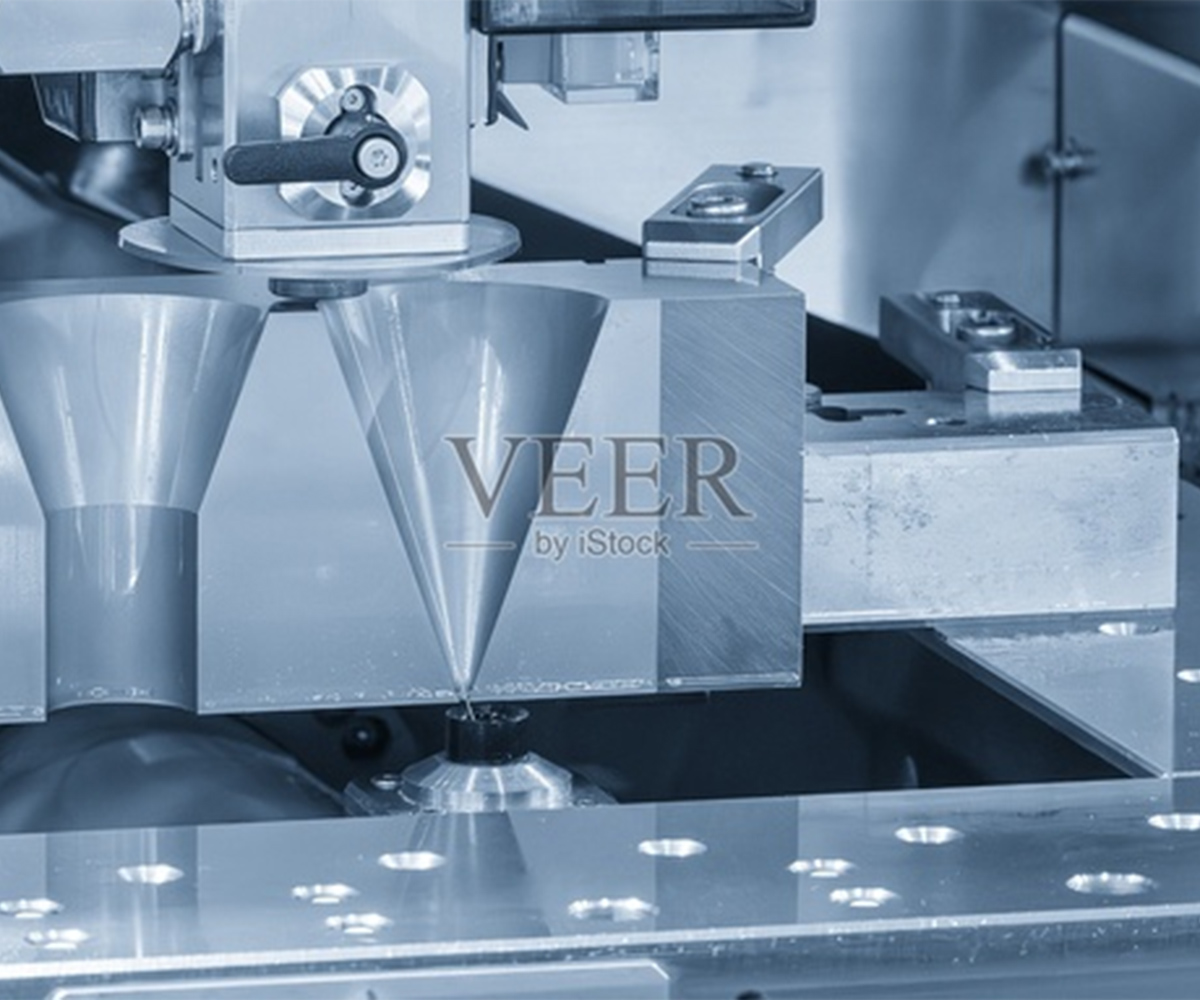
Figure 3: Injection Mold Slider / Angled Ejector Part Machined by Medium-Speed Wire EDM
Brief Summary
The medium-speed molybdenum wire EDM machine is the king of cost-effectiveness in the injection mold industry. It achieves near-slow wire EDM precision at a cost far lower than slow wire EDM, and solves core machining pain points such as high hardness, complex structures, stress-free operation, and zero deformation. In the modern injection mold manufacturing industry, which pursues high efficiency, low cost, and high precision, wire EDM is not only the core competitiveness of small and medium-sized mold factories, but also an important choice for large enterprises to reduce costs and increase efficiency, thus firmly occupying the dominant position in the injection mold processing market.
Product advantages and applicable industries
-
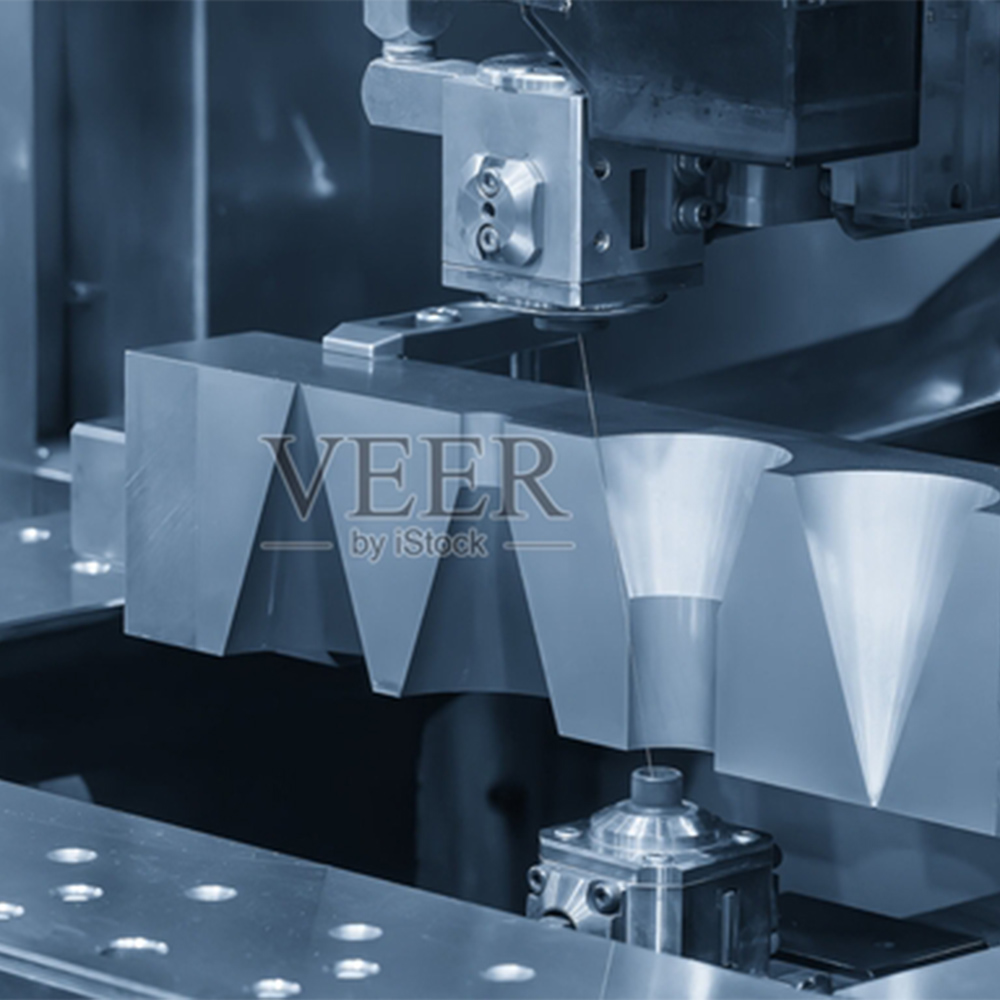
Wire cutting machine tool processing stamping die on site
-
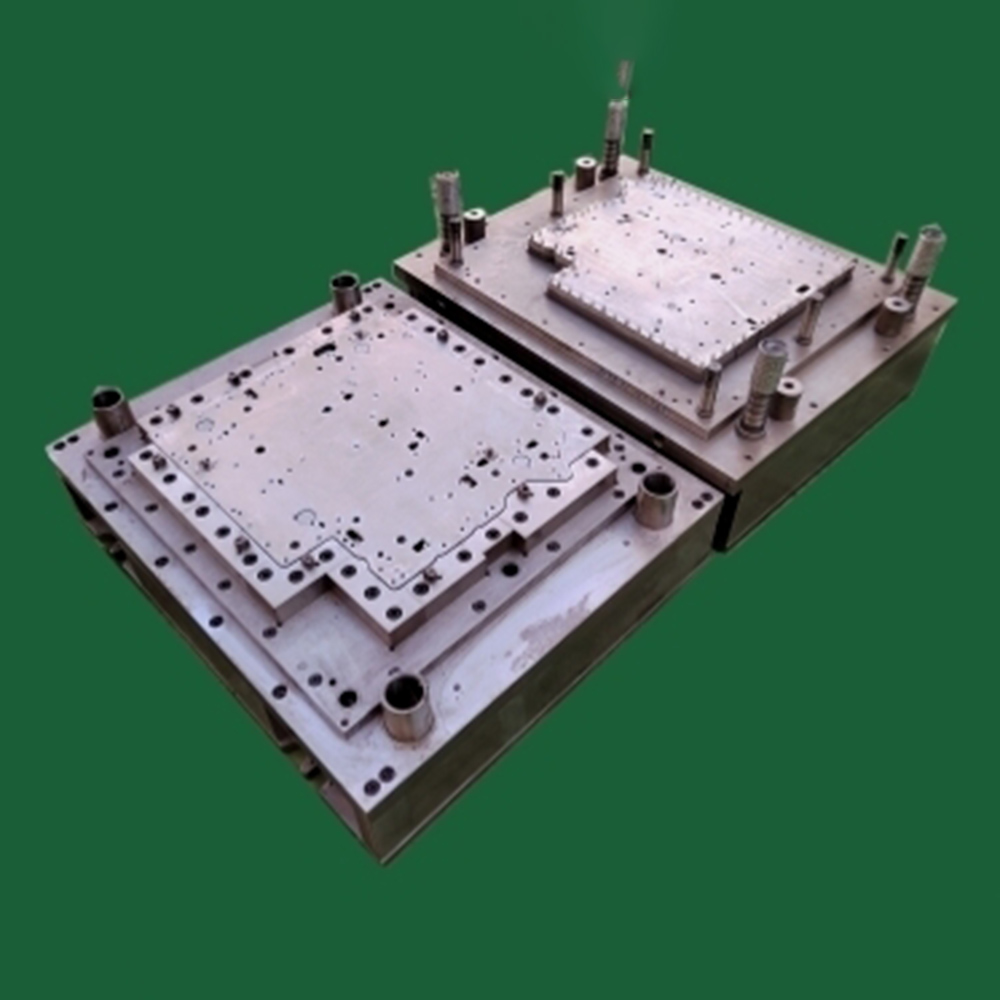
Multi-station continuous stamping die (integrated wire cutting)
-
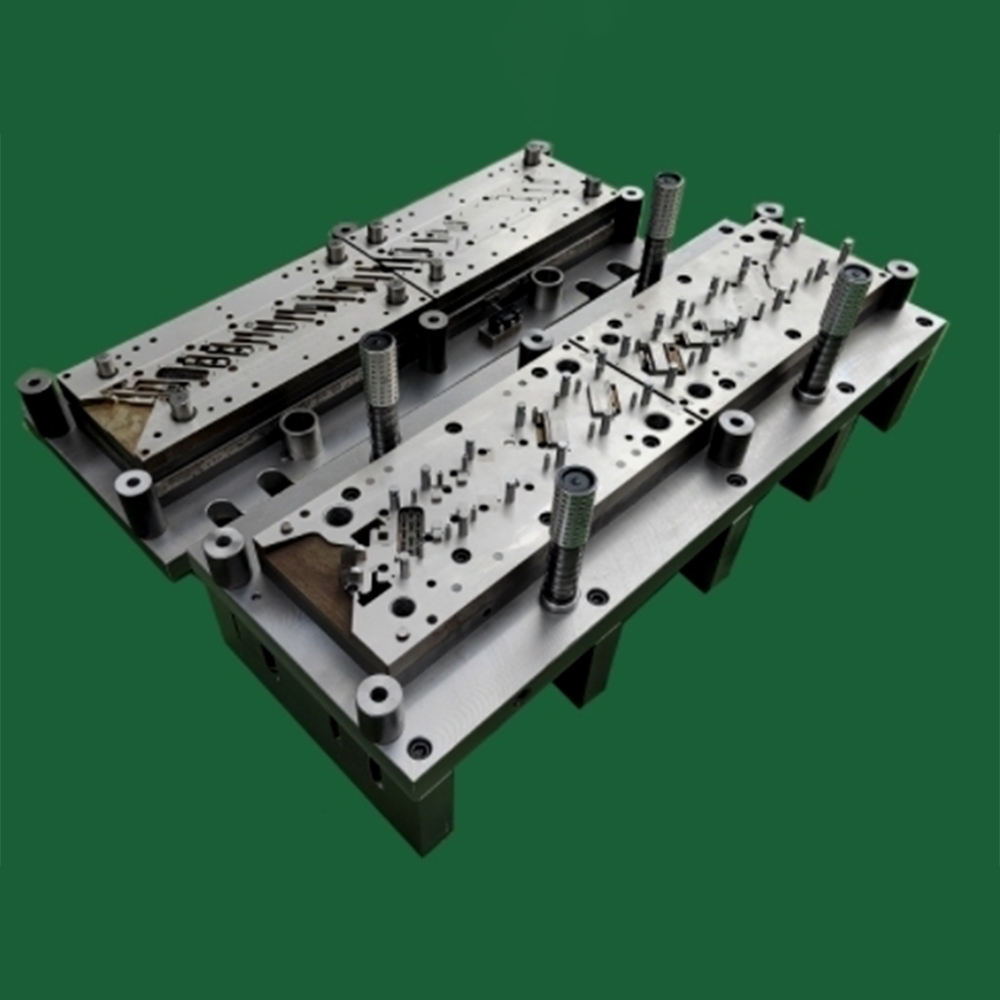
terminal progressive die (typical product of wire cutting)
-
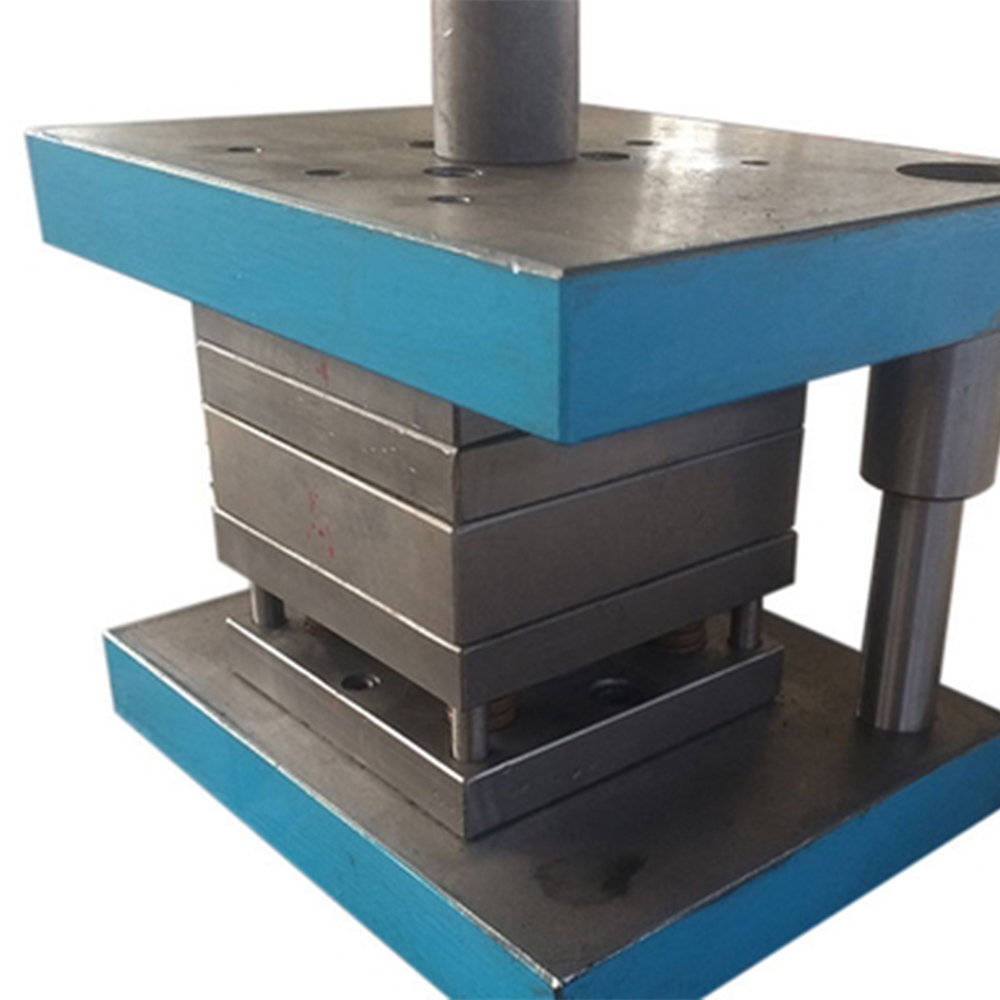
Motor silicon steel sheets, stator and rotor stamping molds (areas where wire cutting excels)